What is bulk density?
Bulk density is the mass of a particulate material divided by the total volume it occupies, including the voids between particles. Particle or true density describes the material inside individual particles and is a different property. Process equipment is commonly concerned with the total volume occupied in a container, on a belt, inside a screw or in a blender, so the two terms cannot be used interchangeably.
The basic calculation is ρb = m / V. The mass m is the net material mass after subtracting the container tare; V is the occupied volume in a defined fill state. Report the result in kg/m³ or t/m³ and always state the units. The formula alone is not a method: particle-size distribution, moisture, aeration, fill height, vibration and resting time can all change the value measured for the same material.
Loose, tapped and process density are different states
For loose or poured bulk density, material is filled into a container by a defined method without intentional consolidation. Tapped density uses a specified tapping or vibration procedure. ASTM D7481 describes loose and tapped measurement with a graduated cylinder for powders and granules within its scope; its sample size and conditions must not be assumed suitable for every material.
Material in a silo, hopper or feeder may be compressed by the load above it. ASTM D6683 therefore treats bulk density as a function of compressive stress. Fine, aeratable powder can show a meaningful difference between its initial density and the density under storage load. One catalogue number or a bench-top container test does not automatically represent a large vessel. Select a method that answers the actual project question.
How should the measurement be planned?
Write down the purpose first: bag volume, conveyor throughput, blender batch volume or storage load? Select a relevant material or sector standard, or a validated laboratory method. A representative sample should reflect normal moisture, particle-size distribution and temperature. Selecting only accessible fines or coarse pieces can bias the result.
Record container volume and geometry, filling device, drop height, levelling technique, number of taps or applied stress, dwell time and ambient conditions. Tare the container, fill it according to the method, determine the net mass and divide by the defined volume. Run several replicates under the same conditions and report the mean and spread. Do not press, shake or aerate the material unless that action is part of the chosen procedure.
A simple calculation example
For illustration only, assume the net mass filling a defined 20-litre volume in the loose state is 12.0 kg. Because 20 litres is 0.020 m³, loose bulk density is 12.0 / 0.020 = 600 kg/m³. If the same sample occupies 17 litres after a standardised tapping procedure, the calculated tapped value is about 706 kg/m³. These figures are not an İnovate machine capacity or product guarantee.
A mass of 3,000 kg would have a theoretical volume of 5.0 m³ at the loose value and about 4.25 m³ at the tapped value. The difference shows why “is the density 600 or 706?” cannot be answered without the state and method. Design also considers working fill, flow behaviour, safety factors and actual process conditions; equipment is not selected from this division alone.
Effect on conveyors, elevators and blenders
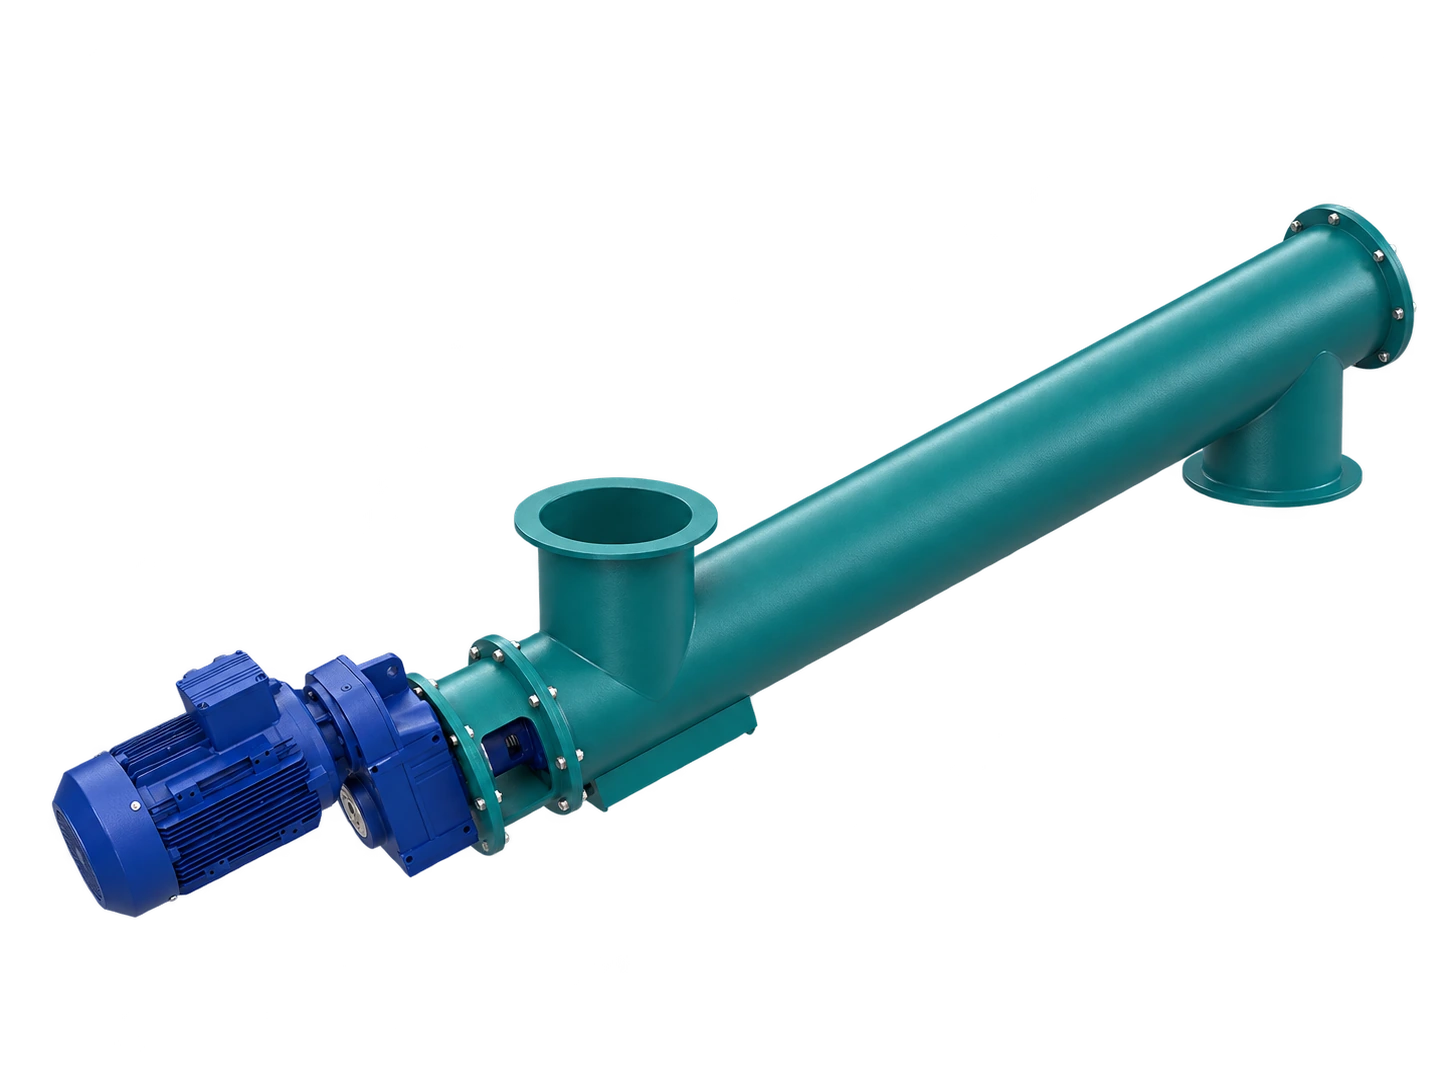
Belt conveyors, screw conveyors and bucket elevators first carry a volumetric flow. A measured bulk density is needed to convert mass flow to volume: m³/h = kg/h ÷ kg/m³. KWS likewise identifies accurate bulk density as necessary when converting between mass and volume in screw-conveyor capacity work. If density is assumed too low, the same tonnes per hour occupy more volume; if it is assumed too high, the required volume can appear smaller than it is.
For a ribbon blender, batch mass is converted to occupied volume using bulk density; ROSS also highlights batch volume and density in blender specification. Loose filling, settlement in the process and aeration during mixing may not be identical states. Share the measured state and a credible range alongside the material name.
What belongs in the project file?
Record material and lot, sampling location and date, moisture, temperature and particle-size distribution, the standard or internal method, the loose, tapped or defined-stress state, container volume, number of replicates, mean and spread. Where possible, provide a reliable range representing different operating conditions. Do not present one value copied from an online table as a measured result.
Do not sample by reaching toward a moving belt, an exposed screw or inside a guard. Use designed sampling points and the site procedure. Where cleaning, clearing or maintenance may expose personnel to hazardous energy, follow the manufacturer instructions and the site energy-isolation and lockout procedure. This article is not an operating instruction.
Sources
Sources were checked on the article publication date. These are general technical references, not documentation of İnovate product specifications.
